On this page12
- Press brake tools at a glance
- Punches (upper tools)
- Dies and bending matrices (lower tools)
- Gooseneck tools for boxes and U-channels
- Steel and hardness
- Machines and systems we make tools for
- Special tools
- Services
- What to send for a quotation
- Where we deliver
- Questions buyers ask
- More about our press brake tools
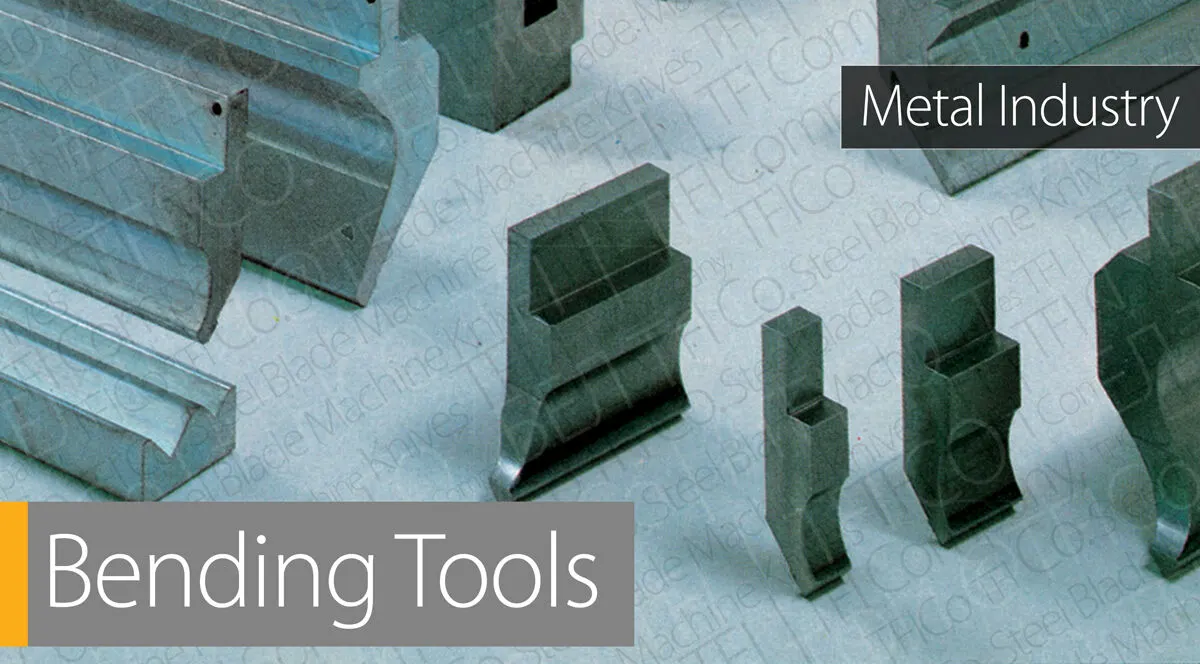
TFI Co. makes press brake tools: the punches (upper tools), dies and bending matrices (lower tools) that shape sheet metal on a press brake. We have made steel blades and machine tools since 1965, and our bending tools fit the machines most workshops run: Euro-style (Promecam / Amada), Trumpf / Wila, Bystronic, LVD, Baykal, Ermak and Hämmerle.
We make standard tools and custom tools to your drawing, including tools for older machines whose original maker no longer supplies them, which we reverse-engineer from your sample.
Press brake tools at a glance
| Feature | What we offer |
|---|---|
| Upper tools | Straight, acute and gooseneck punches, segmented sets, moving horns |
| Lower tools | Single-V, 2V and multi-V dies, bending matrices, rotary (anti-mark) dies, hemming dies |
| Punch angles | 30°, 60°, 85°, 88° and 90° |
| Machines | Euro-style (Promecam / Amada), Trumpf / Wila, Bystronic, LVD, Baykal, Ermak, Hämmerle |
| Steel | High-grade alloy steel such as C45 or 42CrMo |
| Hardness | Working surfaces induction-hardened to 50-60 HRC |
| Lengths | Full length (for example 3150 mm), segmented sets or custom lengths |
| Custom work | Tools made to your drawing or reverse-engineered from a sample |
Upper tools
- What we offer
- Straight, acute and gooseneck punches, segmented sets, moving horns
Lower tools
- What we offer
- Single-V, 2V and multi-V dies, bending matrices, rotary (anti-mark) dies, hemming dies
Punch angles
- What we offer
- 30°, 60°, 85°, 88° and 90°
Machines
- What we offer
- Euro-style (Promecam / Amada), Trumpf / Wila, Bystronic, LVD, Baykal, Ermak, Hämmerle
Steel
- What we offer
- High-grade alloy steel such as C45 or 42CrMo
Hardness
- What we offer
- Working surfaces induction-hardened to 50-60 HRC
Lengths
- What we offer
- Full length (for example 3150 mm), segmented sets or custom lengths
Custom work
- What we offer
- Tools made to your drawing or reverse-engineered from a sample
Punches (upper tools)
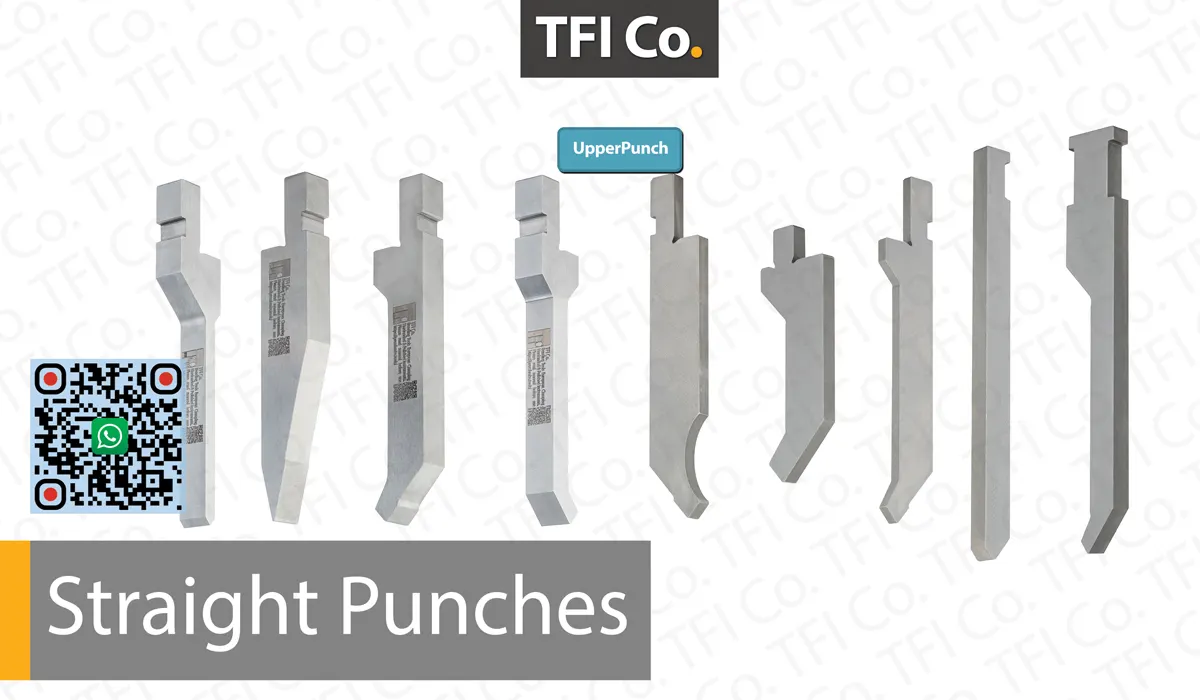
| Punch | Used for |
|---|---|
| Straight punch | Standard bends at 85°, 88° or 90° |
| Acute punch | Sharp angles such as 30° or 45°, and the first step of hemming |
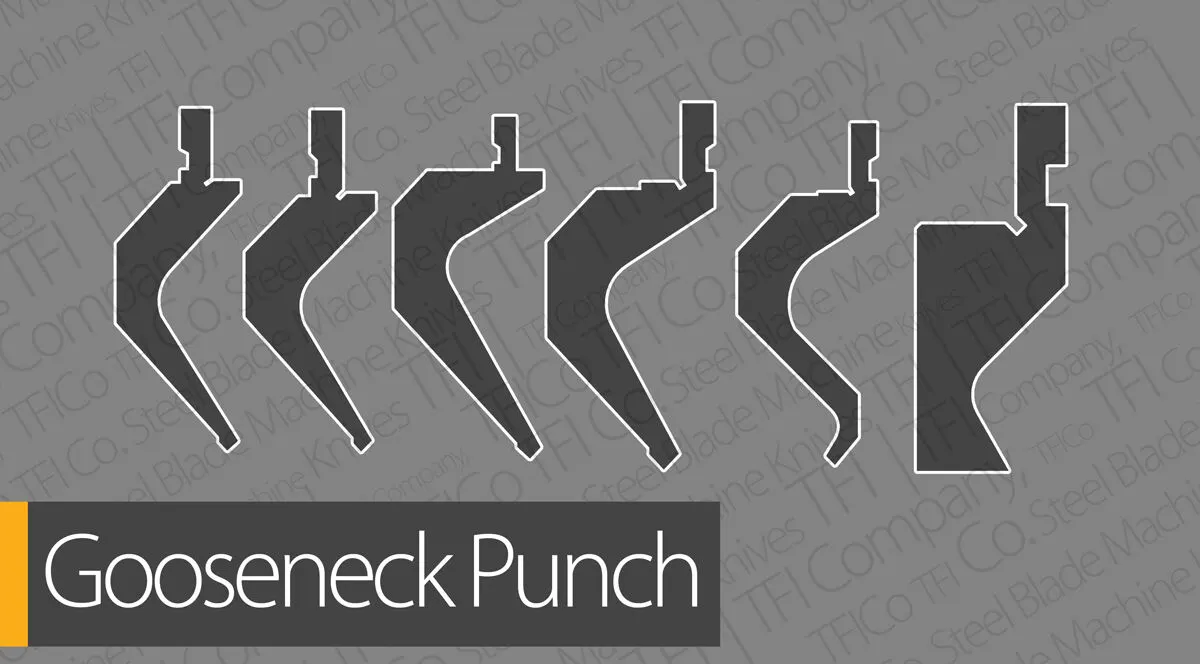
| Gooseneck punch | Deep U-channels and boxes: the curved body leaves room for flanges that are already bent |
| Segmented punch set | Sections of standard lengths combined to match the length of the bend |
| Moving horns | Bending boxes and closed profiles |
Straight punch
- Used for
- Standard bends at 85°, 88° or 90°
Acute punch
- Used for
- Sharp angles such as 30° or 45°, and the first step of hemming
Gooseneck punch
- Used for
- Deep U-channels and boxes: the curved body leaves room for flanges that are already bent
Segmented punch set
- Used for
- Sections of standard lengths combined to match the length of the bend
Moving horns
- Used for
- Bending boxes and closed profiles
Dies and bending matrices (lower tools)
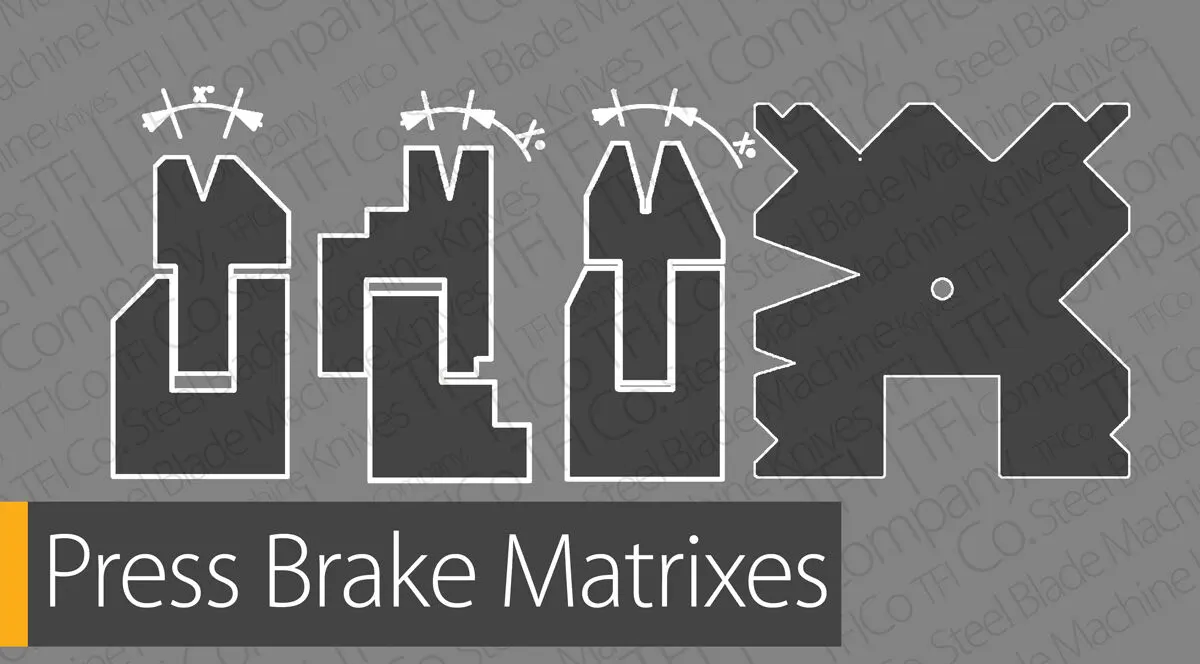
| Die | How it works | Best for |
|---|---|---|
| Single-V (1V) | One V-groove | Many angles and radii; retooling when the job changes |
| 2V die | Two V-grooves side by side | Two bend sizes without retooling; short flanges |
| Multi-V matrix | V-grooves on four sides; rotate the block to change | Many sheet thicknesses with one tool; not for very short flanges |
| Rotary (roller) die | Rotating inserts on both sides of the V | Stainless, aluminium and painted sheet without marks or scratches |
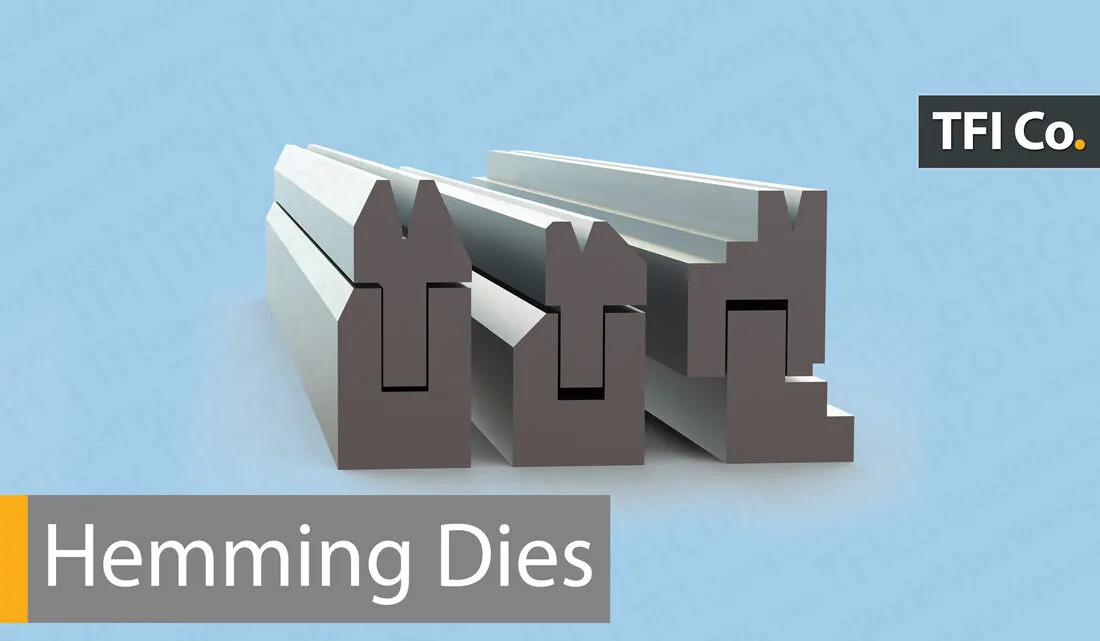
| Hemming die | Flattens a pre-bent flange | Closing and safety hems |
Single-V (1V)
- How it works
- One V-groove
- Best for
- Many angles and radii; retooling when the job changes
2V die
- How it works
- Two V-grooves side by side
- Best for
- Two bend sizes without retooling; short flanges
Multi-V matrix
- How it works
- V-grooves on four sides; rotate the block to change
- Best for
- Many sheet thicknesses with one tool; not for very short flanges
Rotary (roller) die
- How it works
- Rotating inserts on both sides of the V
- Best for
- Stainless, aluminium and painted sheet without marks or scratches
Hemming die
- How it works
- Flattens a pre-bent flange
- Best for
- Closing and safety hems
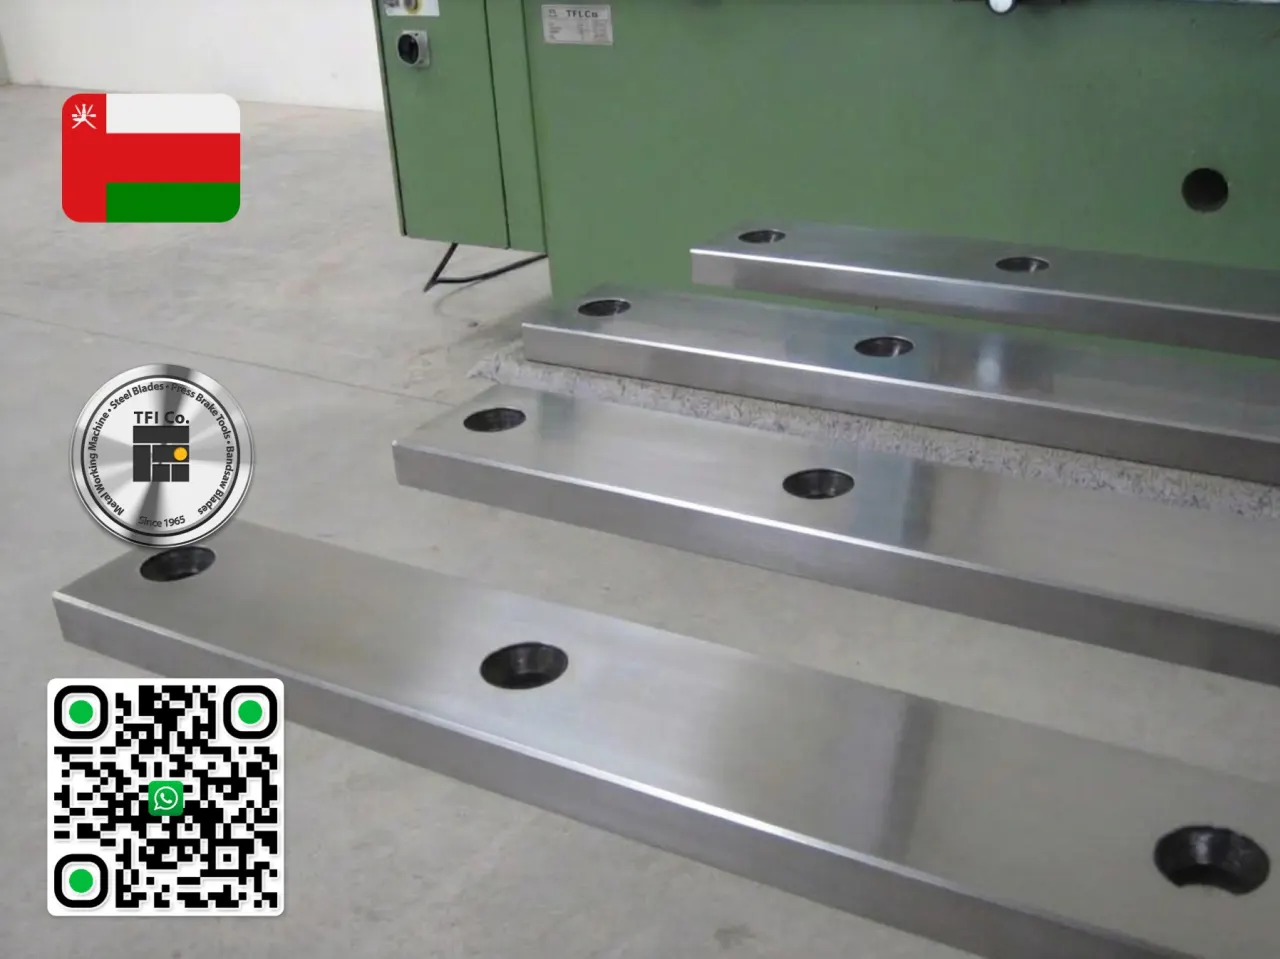
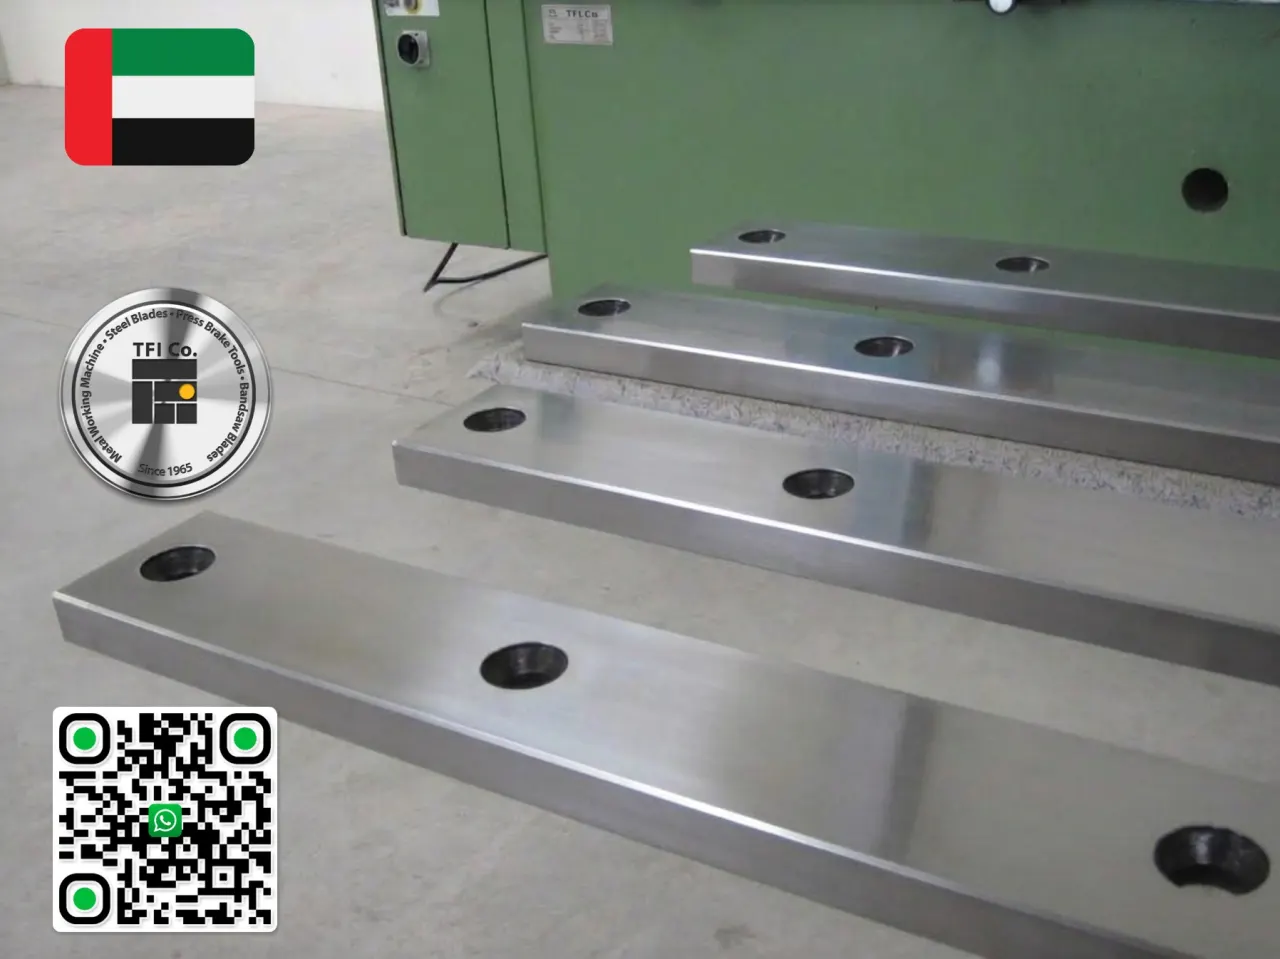
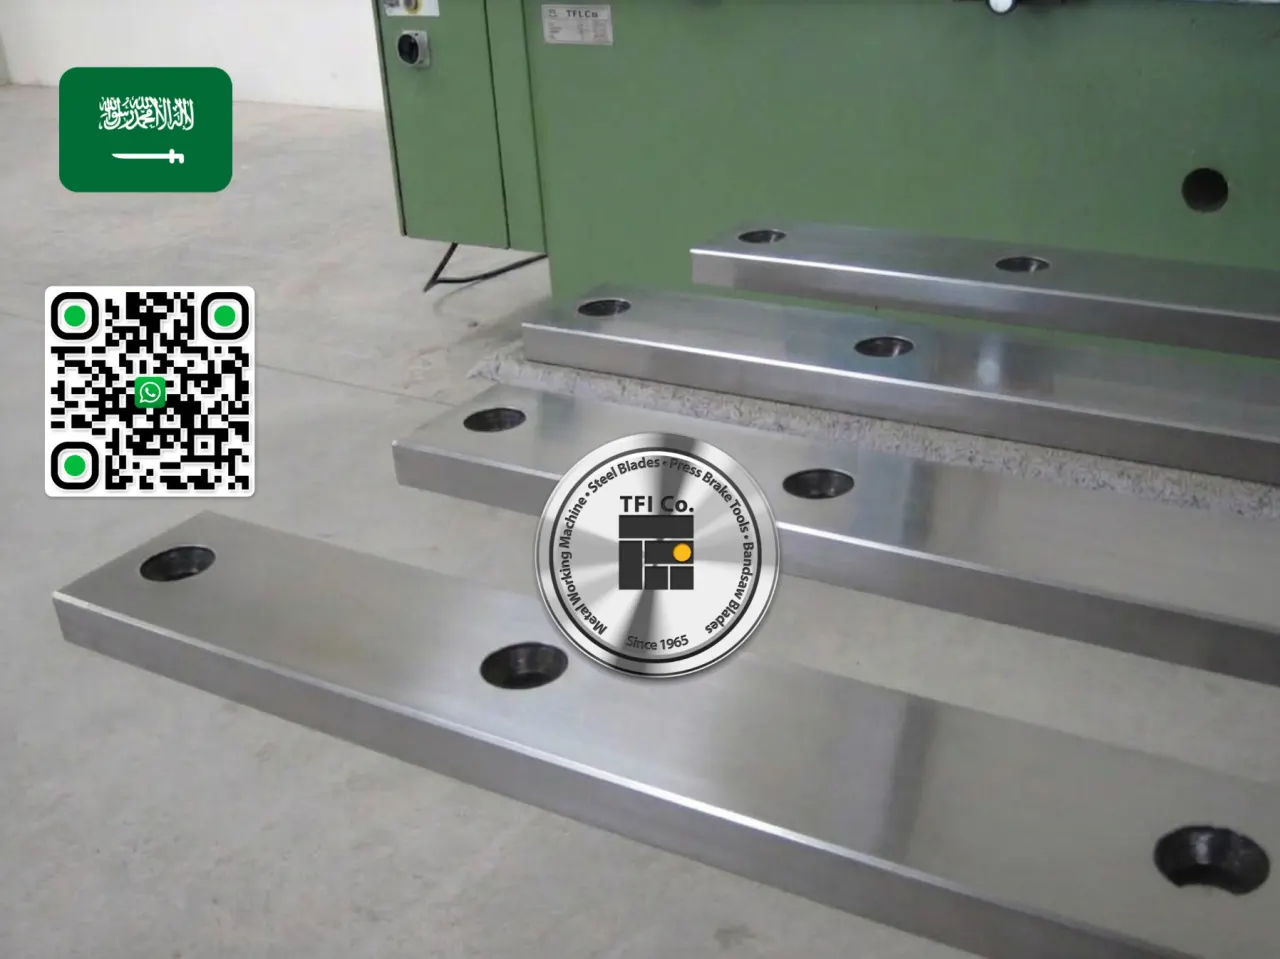
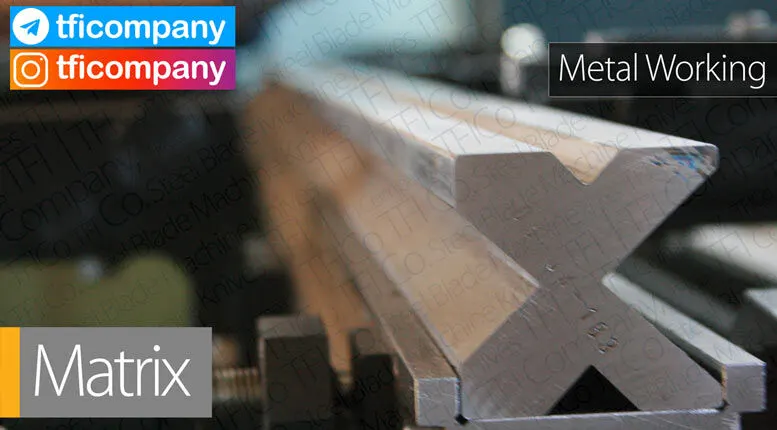
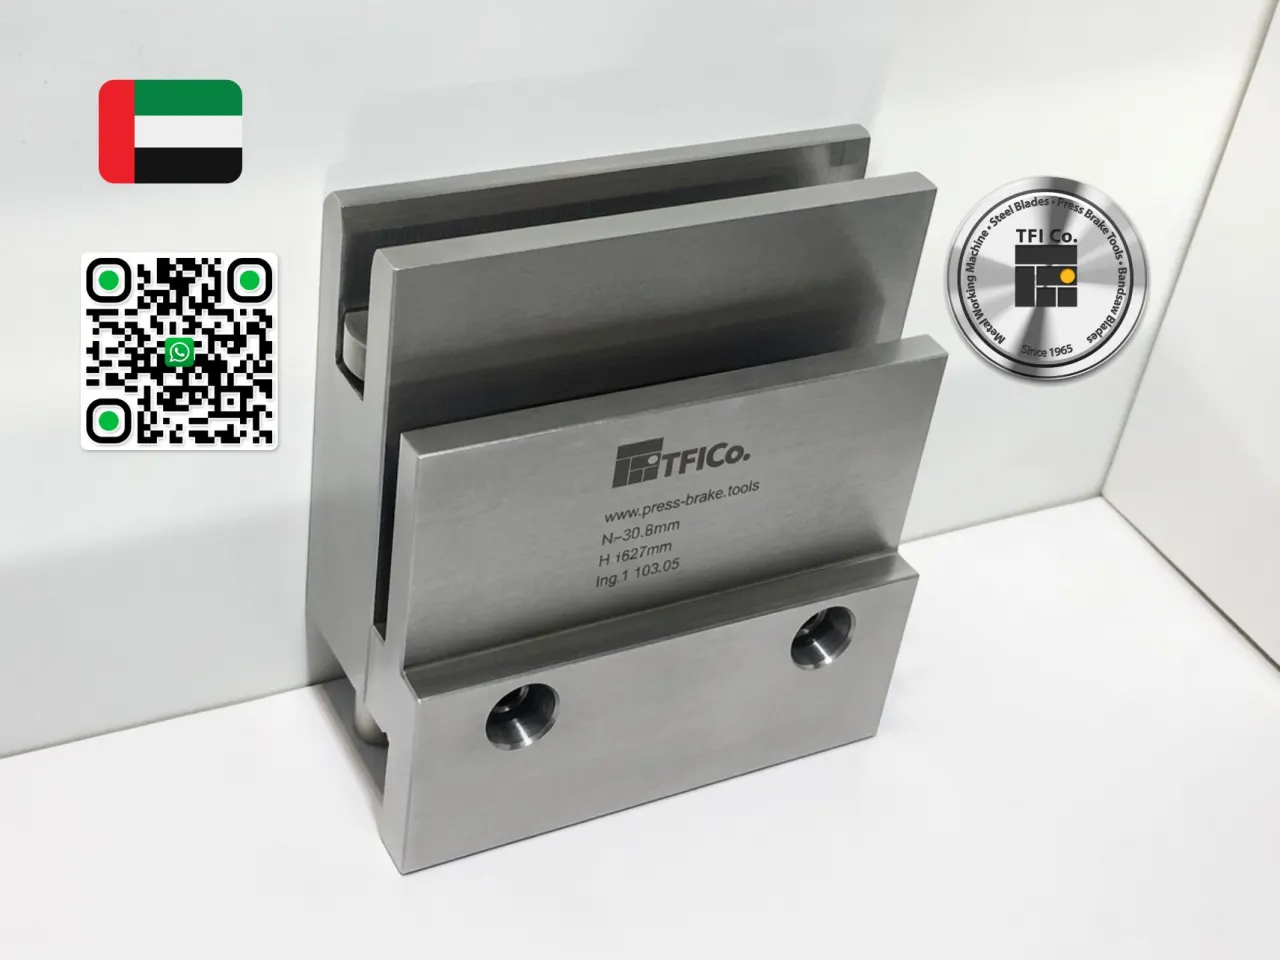
The 4-way bending matrix 95 × 95 × 3150 mm
For 3-metre Euro-style press brakes such as the Promecam 3150, we make a 4-way multi-V matrix with a 95 × 95 mm square section and a 3150 mm length, as one solid piece or in sections. Instead of changing the die for a different sheet thickness, the operator turns the matrix 90° or 180° to the right V-opening.
| V-opening | Sheet thickness |
|---|---|
| V16, V25, V40 | Thin to medium sheet, about 1.5 to 4 mm |
| V63, V80 | Heavy plate, about 5 to 8 mm and more, at 85° or 88° |
V16, V25, V40
- Sheet thickness
- Thin to medium sheet, about 1.5 to 4 mm
V63, V80
- Sheet thickness
- Heavy plate, about 5 to 8 mm and more, at 85° or 88°
Gooseneck tools for boxes and U-channels
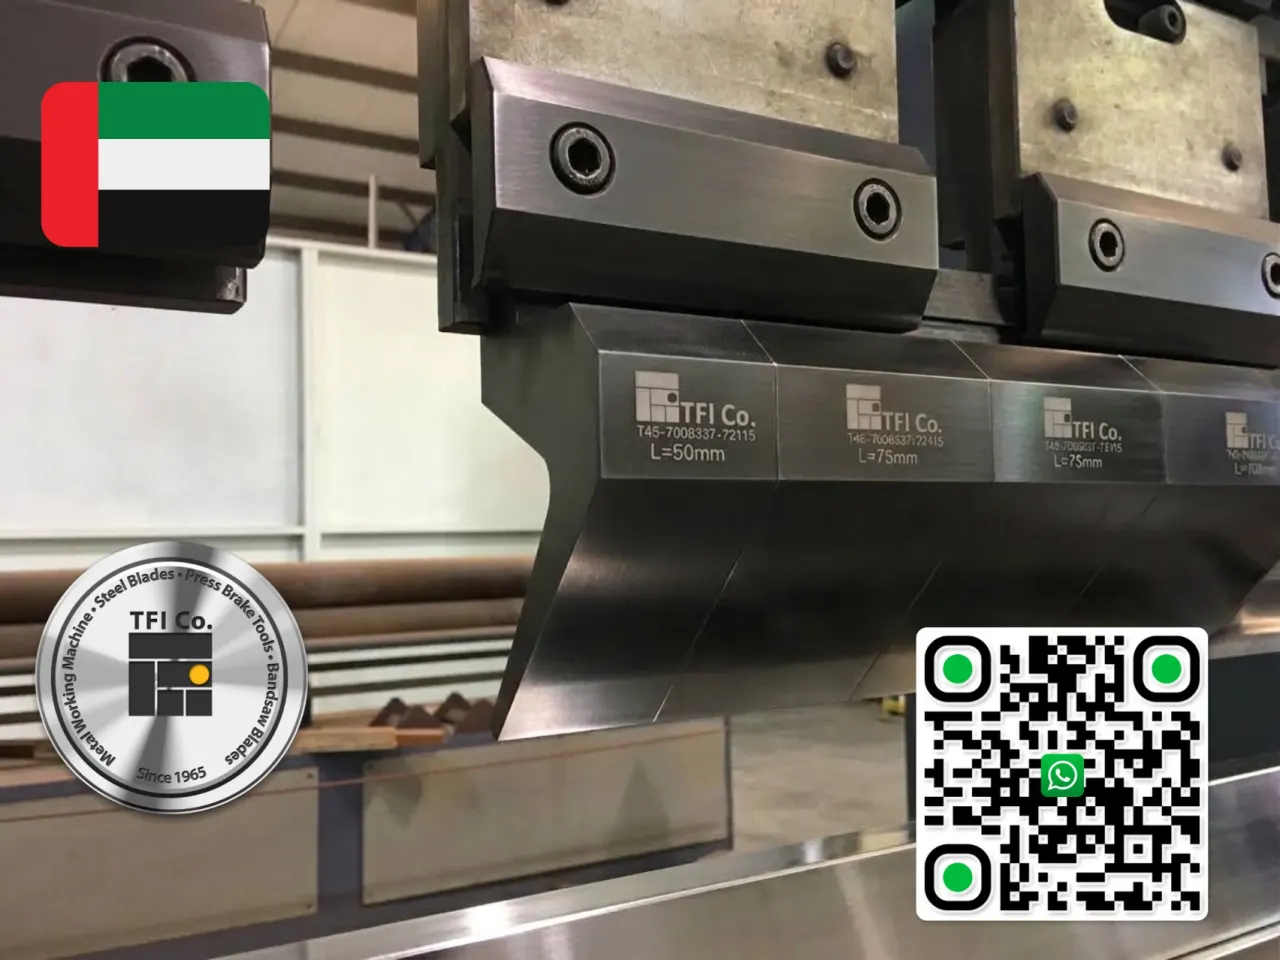
A gooseneck punch has a deep, curved relief in its body, so the sheet does not hit the punch when a flange comes back up. That makes it the tool for deep U-channels, enclosures and boxes bent in several steps. Our EU4416 Euro-style gooseneck punch comes in segmented lengths, so the operator can set up exactly the bending length of the part.
Because the force does not run straight down through the curved body, a gooseneck punch carries less tonnage than a straight punch of the same height. Always check the load limit of the tool for your sheet thickness.
Steel and hardness
Our punches and dies are made from high-grade alloy steels such as C45 or 42CrMo. The parts that touch the sheet, the punch tip and the shoulders of the V, are induction-hardened to 50-60 HRC (52-60 HRC on the V-grooves of a multi-V matrix). The hard surface resists wear, while the tougher core takes the bending load without cracking.
Machines and systems we make tools for
| System | What to know |
|---|---|
| Euro-style (Promecam / Amada) | The most widely used standard. Punches have a safety groove so they cannot drop when the clamp opens; dies sit on a 60 mm wide base. Also fits Accurpress. |
| Trumpf / Wila | Tools for Trumpf and Wila clamping |
| Bystronic | Bystronic-style punches and dies |
| Hämmerle (Bystronic) | 3-point bending tools for very high angle accuracy, reverse-engineered for older machines |
| LVD, Ermak, Baykal | Tools to the machine's clamping, for example an 85° straight punch for Baykal |
Euro-style (Promecam / Amada)
- What to know
- The most widely used standard. Punches have a safety groove so they cannot drop when the clamp opens; dies sit on a 60 mm wide base. Also fits Accurpress.
Trumpf / Wila
- What to know
- Tools for Trumpf and Wila clamping
Bystronic
- What to know
- Bystronic-style punches and dies
Hämmerle (Bystronic)
- What to know
- 3-point bending tools for very high angle accuracy, reverse-engineered for older machines
LVD, Ermak, Baykal
- What to know
- Tools to the machine's clamping, for example an 85° straight punch for Baykal
Special tools
- Hemming and flanging tools for closed edges and flanges.
- Hinge-making, curling and flattening tools.
- Louver punch and die sets for ventilation grilles.
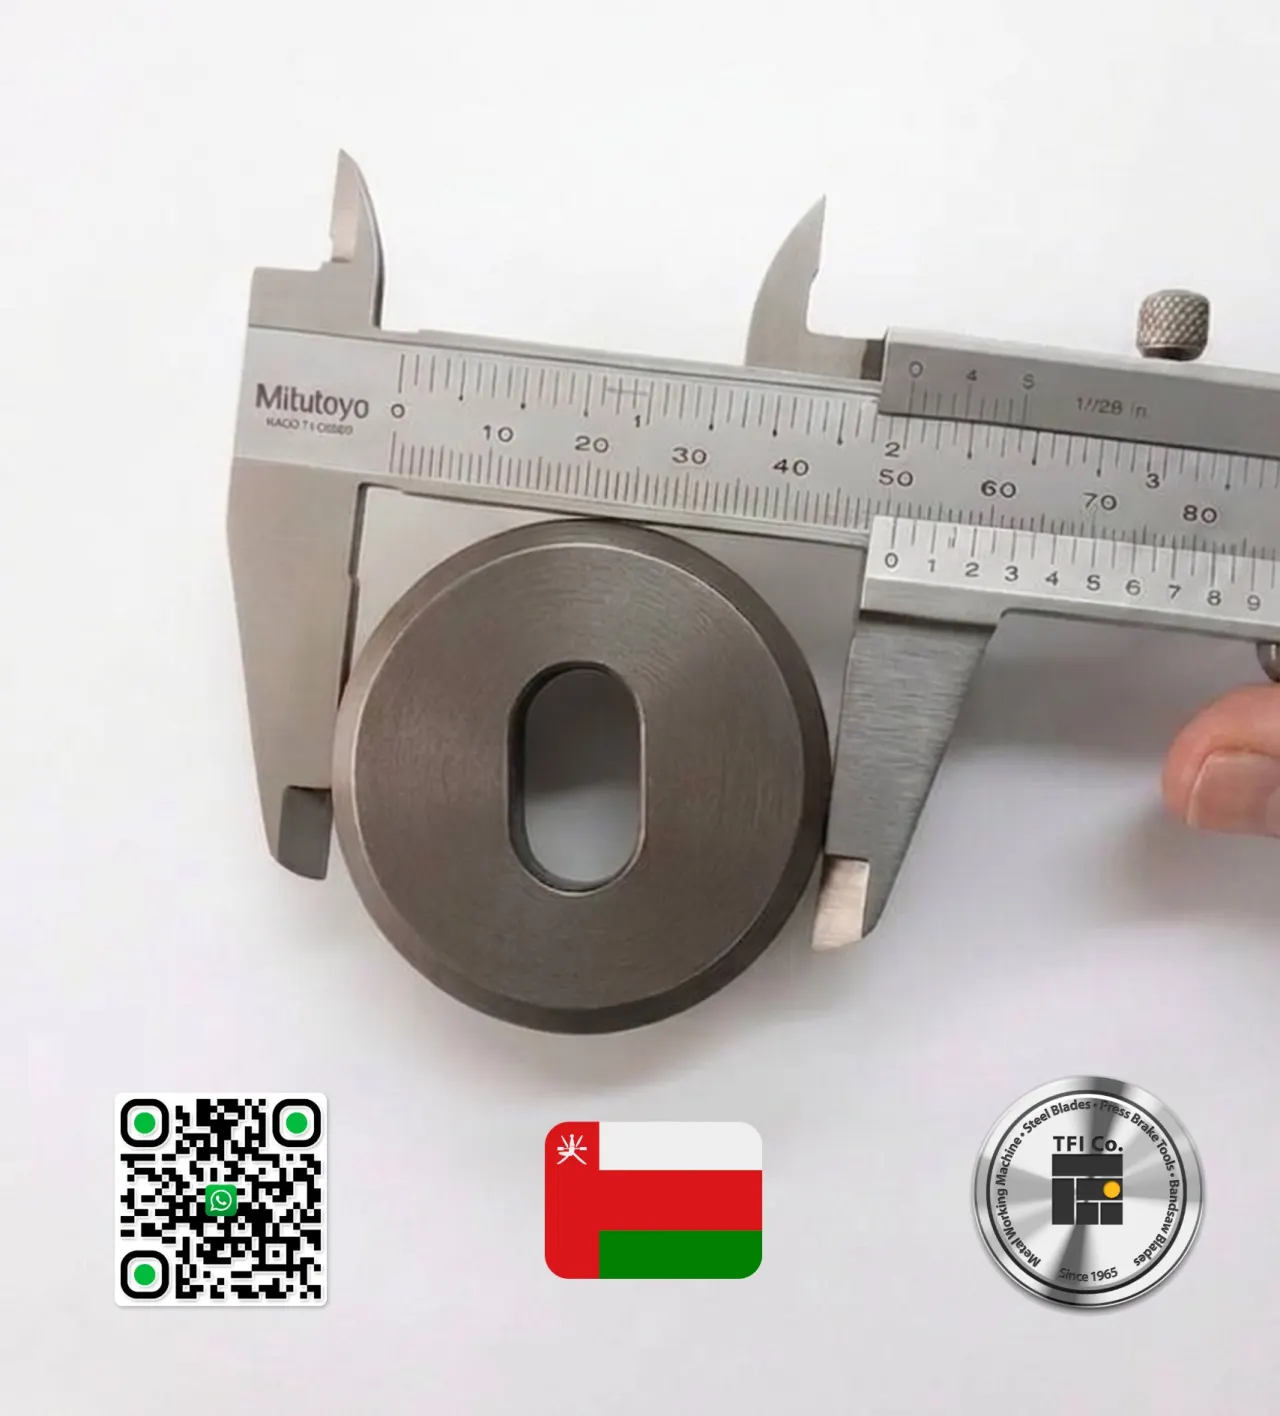
- Punch and die sets for Peddinghaus punching and shearing machines, measured and made to fit the machine's die holder.
- Anti-mark film orange polyurethane film in 30 m rolls that keeps the die from marking the sheet.
Services
- Technical advice on the right tool, V-opening and bend limits for your parts.
- Re-sharpening and reconditioning of worn tools.
- Press brake repair, including hydraulic systems.
What to send for a quotation
| Information | Example |
|---|---|
| Machine make, model and tonnage | Promecam, 100 t |
| Bed length and clamping system | 3150 mm, Euro-style |
| Tool type | Gooseneck punch, multi-V die |
| Angle and V-opening | 88°, V16 |
| Material and thickness you bend | Mild steel, 3 mm |
| Length | Full length or segmented set |
| Drawing or photo with measurements | For custom or older tools |
| Quantity and delivery country | 1 set, Saudi Arabia |
Machine make, model and tonnage
- Example
- Promecam, 100 t
Bed length and clamping system
- Example
- 3150 mm, Euro-style
Tool type
- Example
- Gooseneck punch, multi-V die
Angle and V-opening
- Example
- 88°, V16
Material and thickness you bend
- Example
- Mild steel, 3 mm
Length
- Example
- Full length or segmented set
Drawing or photo with measurements
- Example
- For custom or older tools
Quantity and delivery country
- Example
- 1 set, Saudi Arabia
Request a quotationSend us your drawing on WhatsApp
Where we deliver
We supply press brake tools across the GCC (the UAE, Saudi Arabia, Qatar, Kuwait and Oman) and have delivered to Canada, Belarus, Russia, France, Australia, Japan, Brazil and India, and to other countries on request.
Questions buyers ask
Which tools fit my press brake?
It depends on the clamping system. Most machines use the Euro-style (Promecam / Amada) standard; others use Trumpf / Wila, Bystronic or their own system. Send us the machine make and model, or a photo of the clamp, and we match the tools.
Which V-opening should I use?
As a guide from our 95 × 95 mm matrix: V16 to V40 for sheet of about 1.5 to 4 mm, V63 or V80 for plate of about 5 to 8 mm and more. We confirm the right opening for your material and angle.
What is a gooseneck punch for?
For deep U-channels and boxes: its curved body leaves space for flanges that are already bent. It carries less load than a straight punch, so check the tonnage limit.
Single-V or multi-V die?
A single-V die is simple and suits short flanges. A multi-V matrix has openings on four sides, so one tool covers many thicknesses; you turn it instead of changing it.
Can you make tools for an old machine?
Yes. We reverse-engineer tools from a sample or a drawing, for example for older Hämmerle press brakes and Peddinghaus punching machines.
How hard are the tools?
The working surfaces are induction-hardened to 50-60 HRC on C45 or 42CrMo alloy steel.
More about our press brake tools
- Custom bending tools for Promecam and Amada in Saudi Arabia
- Promecam / Amada bending tools in Oman
- Promecam 3150 bending matrix 95 × 95 mm, Dubai
- EU4416 gooseneck punch, UAE
- Hämmerle press brake tooling, UAE
- Punch and die for Peddinghaus machines, UAE
- Louver punch and die making
- Press brake anti-mark film, Dubai
- Promecam standard punches and dies, Canada
- Shear blades and guillotine knives
- Section
- metalworking
- Updated
- ٥ أكتوبر ٢٠٢٦
- Reading time
- 6 min read
Discuss this with our team
Tell us what you need and our team replies by email.
Send an enquiry